
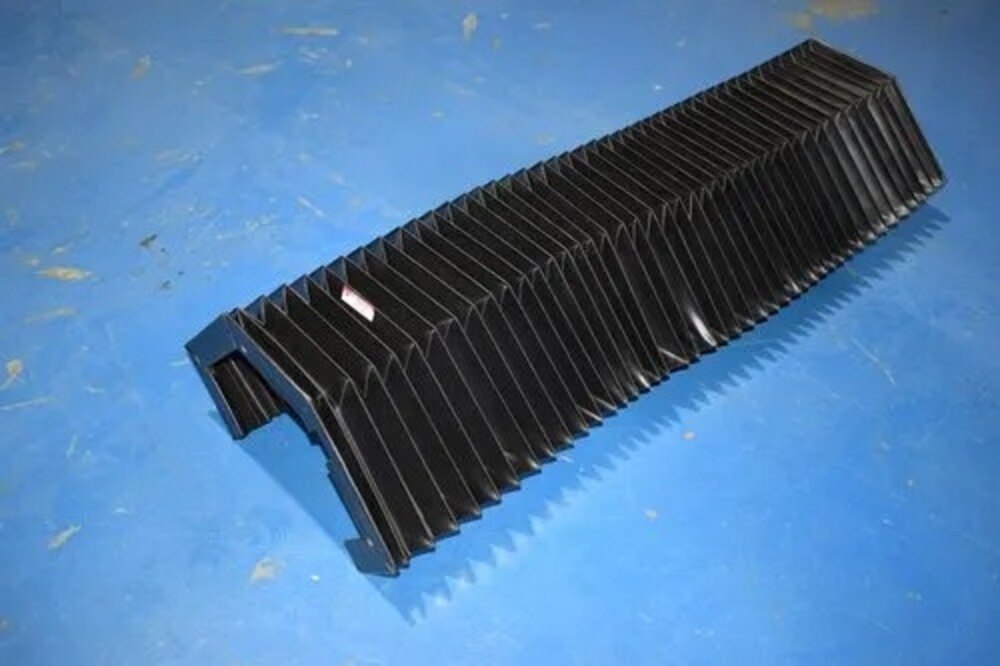
A true bellow exchange cannot be performed safely around moving axes, exposed pinch points or defeated interlocks. You can reduce production interruption by specifying and fabricating the replacement in advance, then completing the physical change during a controlled micro-stop, planned changeover or another machine-specific safe isolation window.
Key takeaways
- Isolate the affected axis before removing any accordion bellow cover.
- Measure compressed length, extended length, mounting points, and travel direction.
- Use temporary shielding to keep debris away from guideways and ways.
- Run a slow, guarded travel test before returning the machine to production.
Decide whether the changeover needs a stop
The practical answer to how to replace accordion bellow covers is to isolate the affected machine or axis, not to work beside moving equipment. A true replacement cannot be performed safely while the axis cycles; defeating an interlock creates crushing, shearing and entanglement hazards.
You can keep the production line running when another machine continues the job, or when the affected machine is taken out during a planned micro-stop or tool-change window. Move the axis to expose the fasteners, isolate its energy, and follow the machine-specific safety procedure before removing the cover.
- Use a planned micro-stop when the replacement is already measured, fabricated and staged with its end frames, retaining strips, fasteners, tools and cleaning materials.
- Keep the rest of the line operating when production can be transferred to another machine or process cell. Treat the isolated machine as unavailable until installation and testing are complete.
- Use a full shutdown and lockout/tagout when access enters the guarded zone, stored energy remains, the axis could move, or the manufacturer’s procedure requires it.
Do not attempt a live exchange with exposed pinch points or a moving axis. An emergency patch can temporarily reduce chip and coolant entry, but it does not restore folding geometry, abrasion resistance or fire behaviour.
Set a replacement deadline, and replace rather than patch crushed pleats, detached frames, exposed guide elements or repeated coolant leaks.
Prepare the replacement and record the installed geometry
A replacement must match the installed geometry, not just the old cover’s overall length. Before removing anything, isolate the machine according to its safety procedure and record the axis position that exposes the fasteners without placing anyone near a moving pinch point.
1. Measure the cover fully compressed and fully extended, then record its width, height, maximum stroke, folded height and clearance from the guideway, ballscrew, spindle, cable carrier and sensors.
2. Measure mounting-hole spacing, hole diameter, flange and end-frame dimensions, retaining-strip size, guide arrangement and the direction of travel. Mark which end faces the fixed frame and which end follows the moving axis.
3. Photograph the cover extended, compressed and at the working axis position. Take close images of both end attachments, fasteners, guide hardware, folds, wipers and any cable or sensor clearance; label each image with the machine, axis and orientation.
4. Write down operating speed and acceleration, coolant type, chip temperature and exposure to oil, UV or flame. These conditions determine the required fabric and construction, so a visually similar cover can still fail quickly.
5. Stage the specified replacement, end frames or retaining strips, new fasteners, supports, torque tools, scrapers, lint-free wipes, approved cleaner and a container for removed hardware. Support the cover’s weight before releasing its attachments.
Confirm the spare against these records before starting the accordion bellow cover replacement. A patch can protect the machine briefly, but set a replacement deadline; it does not restore folding geometry, abrasion resistance or fire behaviour.
Remove the damaged cover without contaminating the machine
A live replacement is unsafe if an axis can move, a cover hides a pinch point, or removing it disturbs a guard, interlock, limit switch or access panel.
Use a planned micro-stop only when the cover section is isolated from production; otherwise apply the machine’s lockout/tagout procedure, isolate electrical, pneumatic and hydraulic energy, and verify zero movement.
1. Move the axis to the recorded access position, stop the spindle, and photograph the cover, end frames, cable carrier and sensor locations. Label the cover’s fixed and moving ends before disconnecting anything.
2. Place clean sheeting over the guideway and ballscrew. Cap an exposed spindle nose, shield sensors, and support the cable carrier with a strap or approved support; never let its weight pull on cables or connectors.
3. Vacuum loose chips around the cover. Use a soft brush and the cover maker’s limits for air pressure, water pressure, temperature and solvents. Do not use sharp hooks, scrapers or uncontrolled high-pressure air, which can drive debris into pleats, seams, bearings or sensor gaps.
4. Support the bellows so fabric carries no load, then remove end frames, retaining strips and fasteners in sequence. Keep hardware in a labelled tray and lift the cover away from the guideway rather than dragging it across the ballscrew.
5. Wipe mounting surfaces clean and inspect for burrs, chips and coolant behind the cover. Keep removed parts away from the cable carrier and sensors until the area is cleared.
6. Fit the replacement without twisting, then hand-cycle the axis through its stroke before restoring power. Recheck every disturbed guard, interlock, limit switch and access panel before operation.
Inspect, install and prove the new cover before production
A new cover will fail quickly if the original cause remains. Treat accordion bellow cover repair as a diagnosis, not a fabric replacement: find the obstruction, misalignment or contamination before fitting the spare.
1. Isolate the axis under the machine’s lockout/tagout procedure. Inspect for sharp chips, burrs, loose fasteners, coolant or chips trapped behind the cover, misaligned way covers, excessive guide friction, incorrect wiper contact and cable-carrier interference. Repair the cause before installation.
2. Compare the replacement with the recorded geometry. Check fully compressed and extended lengths, folded height, width, flange dimensions, mounting-hole spacing, guide position and lateral clearance. Matching the overall length alone will not prevent binding.
3. Clean the mounting faces and install the cover in its photographed orientation. Support its weight with the end frames, not the fabric, then tighten retaining strips or fasteners evenly. Keep every pleat square; a twist at one frame becomes a bind at full compression.
4. With power still isolated, move the axis slowly by hand through its complete travel. Check both axis reversals and full compression for rubbing, trapped pleats, sagging, frame contact and interference with cables, wipers or sensors. Stop and correct any resistance.
5. Restore power only after the machine-specific safety check, then jog at low speed through the same travel and observe the cover from a safe position. Record the final clearance and run a short dry cycle before coolant or chips return.
Include these checks in accordion bellow covers maintenance. Replace rather than patch when pleats are crushed, support layers or stitching are detached, mounting frames are damaged, guide elements are exposed or coolant repeatedly penetrates the cover.
Build a spare-cover process for repeatable near-zero downtime
A near-zero changeover starts weeks before the cover fails. Do not plan a live exchange: moving axes create crushing, shearing and entanglement hazards, so use the machine-specific isolation procedure and lockout/tagout whenever hands enter a pinch point. Exchange the prepared assembly during a planned micro-stop while another machine or production stage carries the work.
1. Create a controlled spare record for each machine and axis. Attach photographs, the drawing, machine ID, axis direction, revision date, mounting orientation, fully extended and compressed lengths, folded height, width, height, hole spacing, flange dimensions and guideway clearances.
2. Specify the conditions, not just the envelope. Record coolant type, oil, chip size, abrasive dust, axis speed, stroke frequency and temperature range. Confirm pleat pitch, guide position, lateral clearance, fabric construction, end frames, wipers and fasteners; matching overall length alone can cause binding at reversal or full compression.
3. Send the measured data sheet to suppliers, including those providing accordion bellow covers in Bangalore. Request an approval drawing and confirm that the complete assembly is available locally. GURUKRUPA BELLOWS PVT LTD can be included in that comparison when its drawing matches the machine’s conditions.
4. Stock the complete, labelled assembly in a clean, dry location, not a bare fabric body. Include replacement hardware and installation tools, then set a review date so a used spare is reordered immediately.
A patch can protect the way briefly, but give it a written replacement deadline; it does not restore folding geometry, abrasion resistance or fire behaviour.
Related product
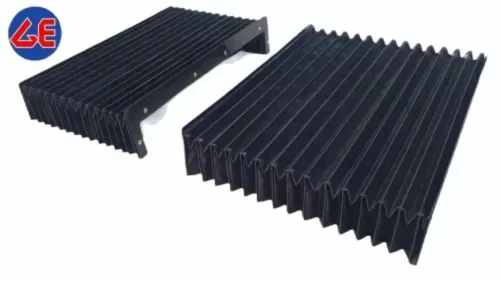
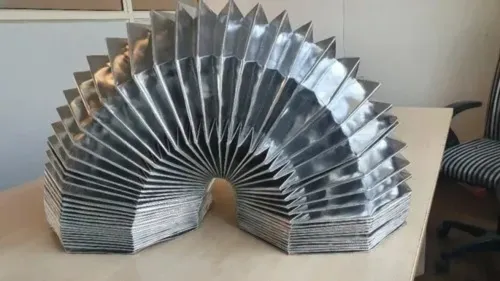
 | Accordion Bellow Cover Ours is a trustworthy name in the business that brings forth Accordion Bellow Cover that is used for delivering controlled pressurized air to a... View product → |
Frequently asked questions
Can you replace an accordion bellow cover while the machine is running?
No. Isolate the affected machine or axis, apply lockout procedures, and never defeat an interlock to work beside moving equipment.
What should you record before installing a replacement accordion bellow cover?
Record compressed and extended lengths, mounting-hole locations, travel direction, attachment method, folds, clearances, and nearby cable or hose positions.
How do you remove a damaged accordion bellow cover without contaminating the machine?
Clean the exterior first, shield exposed guideways, remove fasteners in a controlled sequence, and prevent torn material, chips, and cleaning residue from entering the machine.
How do you prove the replacement cover is ready for production?
Check fastener security and clearances, then cycle the axis slowly through its full travel while watching for rubbing, folding, stretching, snagging, or restricted motion.